Differences Between High-Voltage and High-Current Electrofusion Welders
Posted by Melissa
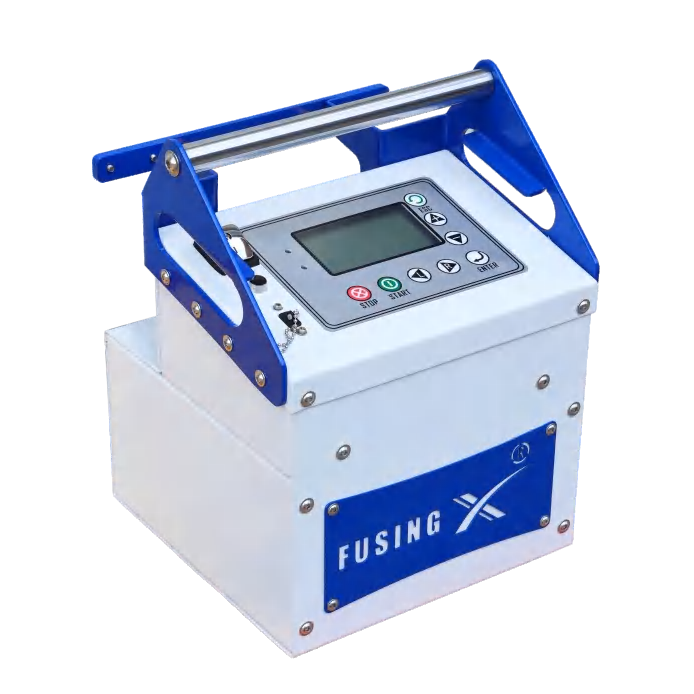
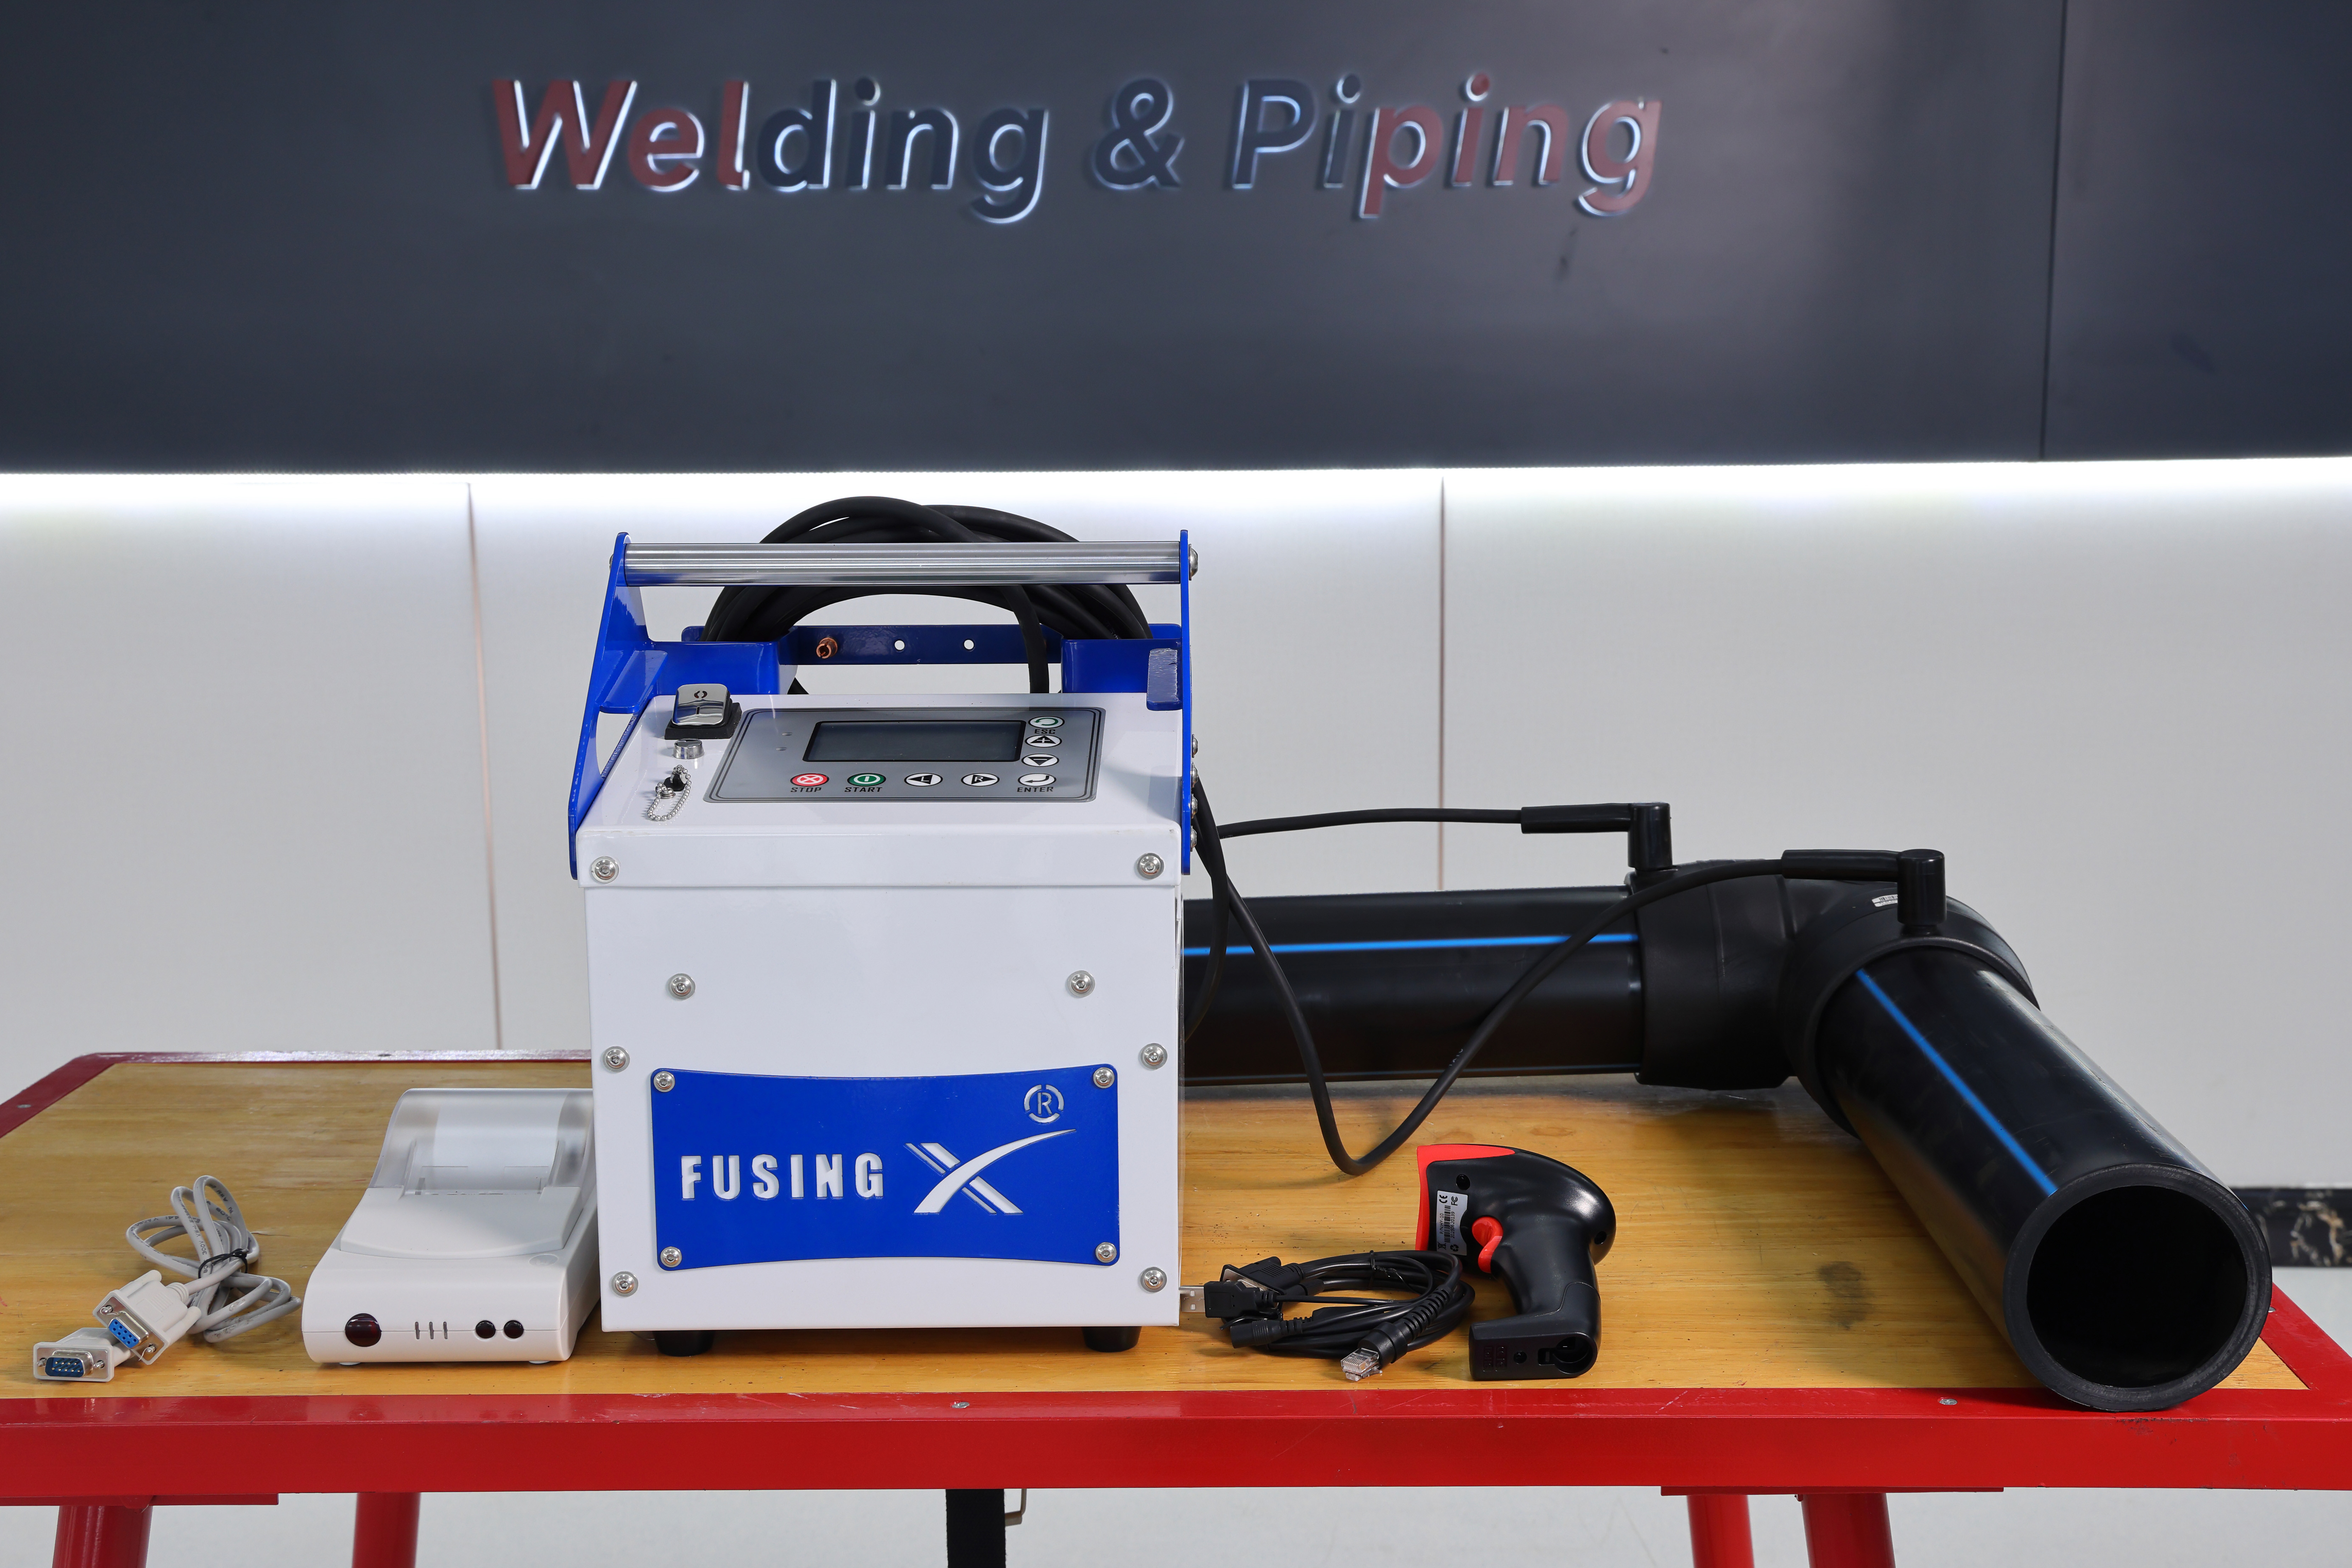
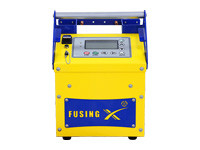
| Model | FX45E(High-Voltage) | FX60E (High-Current) |
| Welding mode | automatic and manual | automatic and manual |
| Suitable material | PE, PP | PE, PP |
| Reference welding range | 20-630mm | 20-630mm |
| Power supply | 220V±10%, 50-60Hz | 220V±10%, 50-60 Hz |
Power | 6000w | 6000w |
Ambient temperature | -15~45℃ | -15~45℃ |
Output voltage | 3~95V | 10~60V |
Output current | 3~60A | 10~90A |
Control mode | Constant voltage / Constant current | Constant voltage / Constant current |
Data record | 500 | 500 |
Duty rate | 60% | 60% |
Data interface | Standard scanner, USB port, optional: printer | Standard scanner, USB port, optional: printer |
| Item | FX45E (High-voltage type) | FX60E (High-current type) |
| Positioning | Higher output voltage with medium current; voltage headroom covers high-resistance loads | Lower output voltage with large current; current headroom covers low-resistance loads |
| Output range | 3~95V / 3~60A (both adjustable) | 10~60V / 10~90A |
Power matching | 6000W; rated point approx. 95V×60A ≈ 5.7kW (headroom on voltage side) | 6000W; rated point approx. 60V×90A ≈ 5.4kW (headroom on current side) |
| Power supply | 220V±10%, 50-60Hz | 220V±10%, 50-60Hz |
Control mode | Constant voltage / Constant current | Constant voltage / Constant current |
Fusion range | 20-630mm | 20-630mm |
Fitting match | Large-diameter, thick-wall fittings with long, high-resistance heating wires: large couplers, large elbows, flange fittings | Small-diameter, low-resistance fittings that need high current density: saddle fittings, in-line fittings, small-diameter couplers |
Output behaviour | Voltage-priority. On long loops and high-resistance loads, the 95V ceiling still drives the rated current; extra margin to offset voltage drop when welding cables are extended | Current-priority. On low-resistance loads it builds 90A quickly, giving fast heat-up and a short fusion cycle |
Advantages | 1. 95V voltage ceiling pushes rated current even through long heating wires of high-resistance fittings — strong all-round coverage of 20-630mm
2. On site with extended cables and large voltage drop, the voltage range compensates line loss and keeps the cycle stable
3. Constant-voltage setting is intuitive; with barcode scanning it matches the fitting's rated voltage directly
4. One machine covers small to large diameters, simplifying model selection for customers | 1. 90A current ceiling heats low-resistance fittings fast, giving full penetration and a uniform joint
2. 60V output ceiling is safer for small fittings and greatly reduces the risk of burning out the heating wire
3. High-current short-time process raises efficiency on thick-wall, wide fittings
4. Ample current headroom — no power derating during long high-current cycles |
Limitations | 1. With 6000W the maximum current is only 60A; low-resistance small fittings that need 90A are out of reach
2. Small fittings run at a high voltage step cannot reach the required current, so a lower step must be used and efficiency drops
3. Short heating wires can overshoot on the highest voltage step, requiring precise voltage setting | 1. The 60V ceiling may fail to reach rated current on large fittings with long heating wires; large-diameter joints are more demanding
2. With long cables the voltage drop of a high-current output is more noticeable — stricter limits on cable length and cross-section
3. High-current low-resistance work depends heavily on contact resistance and clamp quality; poor contact can burn the terminals |
Field notes | Prefer for large diameters and long welding cables; do not use the highest voltage step on small fittings | Prefer for small diameters and short cables; watch cable cross-section and length to avoid current shortfall from voltage drop |
Recommended use | Urban gas and water networks, 20-630mm large-diameter electrofusion fittings; sites with long cable runs and unstable power supply | Confined-space small fittings, saddle branches, fast repair and emergency fusion; thick-wall parts requiring fast high-current fusion |
Selling point (EN) | High-voltage output up to 95V with 60A rated current — holds full rated current on long heating wires of large-diameter fittings and tolerates voltage drop on extended welding cables. | High-current output up to 90A at a maximum of 60V — fast heat-up and full fusion on low-resistance fittings such as saddles and small couplers, with better protection against wire burnout. |
Terminology note | "High-voltage type / High-current type" here refers to output-side voltage-current matching only. The fusion process is constant-voltage or constant-current heating, not the millisecond pulse discharge of metal capacitor-discharge (CD) welding. | Same as left: output matching design; continuous constant-voltage/constant-current heating, not pulse discharge. |